Independent comparisons. We may earn from shop links. More info

How to use a gasless MIG welder

Updated: October 2026

The first bead usually fails before the metal is the problem. The wire nests inside the feeder, the arc crackles because the polarity is still set for solid wire, or you strike without a filter. How to use a gasless MIG welder, on the inverters in this set, starts with the machine off, the wire packet in your hand, and a clear bench. The [flux core wire welder comparison](/hub/soldering-and-welding/flux-core-wire-welder) is where the five listings sit. This page is the setup, not a ranking. The steps follow public UK guidance and these amazon.co.uk kits, as held on 16 October 2026. We did not film a weld. A qualifying purchase can earn a commission at no extra cost to you.

The first bead usually fails before the metal is the problem. The wire nests inside the feeder, the arc crackles because the polarity is still set for solid wire, or you strike without a filter.

Our top picks

HITBOX HITBOX HBM200

Best overall

HITBOX HITBOX HBM200
9.1/10about £99.99
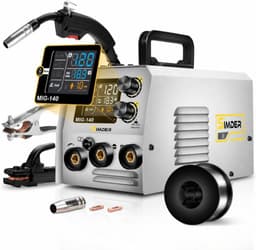
SSimder SSimder MIG-140

Best value

SSimder SSimder MIG-140
8.9/10about £79.99
HITBOX HITBOX HBM1200

Alternative

HITBOX HITBOX HBM1200
8.1/10about £149.99
On this page

Before the spool goes in

Put the filter on before you care about the spool tension. Eye and face protection for welding sits under BS EN ISO 16321-2. None of the five included-component lists names a helmet. A pair of sunglasses is not a substitute, and a grinding visor is not a welding filter. HSE also expects gloves, and goggles when you chip slag, because the chip comes off hot. Fume is the other thing to arrange while the machine is still cold. HSE treats mild-steel welding fume as a hazard for any duration. Indoors, that means local exhaust. Outdoors, or where extraction cannot cope, you still need suitable respiratory protection. Earth the work on bare metal, close to the joint, not on paint. If you are learning, cut mild steel around 3 mm, thicker than a car wing. If the breaker is what stops you, that limit is on the buying guide. HBM1200 reviewers say the manual does not explain feeding. You will set polarity from the wire packet, and find a usable voltage on scrap.

Polarity and rolls

Most self-shielded flux-cored wire runs DCEN, electrode negative. A UK reviewer of the SSimder MIG-140 described the earth clamp on the positive terminal for flux core: the torch is negative, the work is positive. Gas-shielded wire, and ordinary solid MIG wire, are often the other way, DCEP. The packet overrides the habit. Do not swap the leads while the set is live. Wrong polarity gives you spatter, a tall rope of wire, or a weld that sits on the surface. Flux-cored wire is a tube. Hobart’s spool guidance asks for a V-knurled roll and light tension, enough to drive the wire and not enough to crush it. If this feeder has a smooth roll fitted for solid wire, and the tube slips or flattens, fit the knurled roll before you blame the motor. Match the contact tip to the wire. A PLASMARGON review describes a 0.8 mm tip used with 1 mm wire, which is how you get burn-back. If the included spool is 0.8 mm, the tip for the first hour should be 0.8 mm too.
HITBOX HITBOX HBM200

Testsieger

HITBOX HITBOX HBM200
9.1/10about £99.99

Loading the wire

Unplug the set before your hands are in the feeder. Sit the spool so it unwinds the way the diagram shows, and keep a thumb on the free end. Feed the end across the roll and into the liner with the torch as straight as the cable allows. Jog the wire with the torch pointing at the floor, away from your hand and away from the earth clamp. If it kinks inside the roll housing, you have a bird’s nest. Cut the damaged end, rethread, and ease the tension rather than clamping harder. More tension makes a crushed tube, and a crushed tube nests again. On a gasless-only machine the shroud is mostly a spatter shield. On the SSimder MIG-250, which also claims gas MIG, do not remove parts because a forum said visibility was better. The included spool is a starter. HBM1200 reviews say the supplied wire snaps. If the first metre breaks in the roll, bin that spool and load a known 0.8 mm self-shielded wire. Keep the packet. You still need its polarity line.

The first bead and the slag

Lay the scrap flat, clamp it, and drag, so the slag freezes behind the arc. A push on flux core often leaves slag in the weld. Start at the knobs near the bottom of their travel. If the wire stubs into the plate, add a little voltage or ease the speed. If it burns back into the tip, you are too hot or too slow, or the tip is the wrong size. The PLASMARGON may not give you a separate wire-speed knob, so you change the one control it does give you and you watch the puddle. Weld a short bead and stop. Chip the slag once it has cooled, wearing goggles, and brush back to bright metal before the next pass. A usable scrap bead is a consistent width, slag that releases, and metal that joined. It is not a structural sign-off. If the plate is falling through, that thickness belongs on the car bodywork page. Stop and get help if the plug or the lead is hot, if you are about to weld a sill or a seat-belt anchor, if you are inside a tank, or if the wire still will not feed after a fresh spool, a correct tip and a knurled roll.

Common questions

What polarity do you set for gasless flux-core wire?
For most self-shielded wire, DCEN: torch negative, work positive. A SSimder MIG-140 review describes the earth clamp on the positive terminal for flux core. Gas-shielded wires are often the opposite. Unplug the machine and follow the packet in your hand, including when you replace the included spool.
How do you load a spool without a bird’s nest?
Keep hold of the free end, feed it across a knurled roll with light tension, and jog it through a straight torch lead. If it tangles in the housing, cut it, rethread, and reduce tension. Crushing the tube to grip it makes the next nest more likely. Match the contact tip to the wire diameter before you try to weld.
Do you push or drag?
Drag, so the slag stays behind the puddle. Pushing self-shielded wire tends to leave slag in the bead. This is the usual FCAW habit from training notes such as Leeds Engineering. It is not a voltage setting, and it does not fix wrong polarity.
Why is there slag, and when do you chip it?
The flux in the wire forms slag as well as gas. That crust has to come off before the next pass, or you weld over it. Chip once the bead has cooled enough to handle, wearing goggles, and brush back to clean metal. Gas MIG with solid wire does not leave this crust. Flux core does, every pass.
What if the wire burns back or will not feed?
Burn-back into the tip usually means the tip is too small or too close, or the wire speed is too low for the voltage. A refusal to feed is often a crushed wire, a kinked liner, or the smooth roll still fitted. HBM1200 reviews also blame the included spool for snapping. Change to a sound 0.8 mm self-shielded wire before you condemn the motor. Do not keep the trigger down on a stalled roll.
What PPE is not in these boxes?
A welding helmet is not in the included lists of the five. Gloves and slag goggles are your problem too. Eye protection needs to meet a welding filter standard such as BS EN ISO 16321-2. You also need a way to control fume, which HSE treats as local exhaust indoors and respiratory protection outdoors. The kits are a power source and a torch, not a safe setup.

Related pages

Sources

Public UK sources and the amazon.co.uk listings in this set, last checked on 17 October 2026.

  1. HSE, mild steel welding fume (retrieved 17 October 2026)
  2. HSE, welding controls (retrieved 17 October 2026)
  3. HSE WL3, welding fume (retrieved 17 October 2026)
  4. BS EN ISO 16321-2:2021, eye and face protection for welding (retrieved 17 October 2026)
  5. Basic Welding, what duty cycle means (retrieved 17 October 2026)
  6. Sealey MIG140i instructions (retrieved 17 October 2026)
  7. TWI, flux-cored arc welding FAQ (retrieved 17 October 2026)
  8. GOV.UK MOT inspection manual, appendix A (retrieved 17 October 2026)